OSHA’s Process Safety Management standard (29 CFR 1910.119) applies to facilities handling highly hazardous chemicals above threshold quantities. PSM is not just a regulatory checkbox — it is a systematic approach to preventing catastrophic releases that injure workers, damage communities, and destroy facilities. Explosions like Texas City (2005) and fires like the one at Chevron Richmond (2012) consistently trace back to failures in one or more PSM elements.
Who Must Comply with PSM?
A facility is covered by OSHA PSM if it handles any OSHA-listed highly hazardous chemical above its threshold quantity (TQ), or any flammable liquid or gas in quantities exceeding 10,000 pounds. Common covered chemicals include chlorine, ammonia, hydrogen fluoride, hydrogen, methane (in large compressed quantities), and dozens of others listed in Appendix A of 29 CFR 1910.119.
Industries most commonly subject to PSM include chemical manufacturing, petroleum refining, natural gas processing, wastewater treatment, pulp and paper, food processing (ammonia refrigeration), and utilities (chlorination systems). If you are unsure whether your facility is covered, compare your maximum inventory to the OSHA threshold quantities table — a covered quantity is any amount above the TQ, not just the amount present at one time.
The 14 Elements of OSHA PSM
OSHA PSM defines 14 elements, each covering a specific aspect of process safety management:
- Process Safety Information (PSI): Compile and maintain written information on the hazards of chemicals used (physical properties, reactivity, toxicity), process technology (block flow diagrams, process chemistry, operating limits), and equipment (piping and instrumentation diagrams, electrical classification, equipment specifications). PSI is the foundation everything else is built on.
- Process Hazard Analysis (PHA): Conduct a structured review of process hazards using a recognised methodology — HAZOP (Hazard and Operability Study), What-If, FMEA, or fault tree analysis. PHAs must be done for all covered processes and reviewed every five years. Action items from PHAs must be resolved and documented.
- Operating Procedures: Develop and maintain written operating procedures for startup, normal operations, temporary operations, emergency shutdown, and normal shutdown. Procedures must be accessible to operators and reviewed at least annually for accuracy.
- Training: Train employees on the process hazards, operating procedures, and safety systems. Initial training is required before independent work on covered processes; refresher training every three years. Training must be documented with the employee’s name, date, and means used to verify understanding.
- Contractors: Evaluate contractor safety performance and provide contractors with information on the hazards of the processes they are working near. Contractors are responsible for training their own employees, but the facility owner must verify this was done.
- Pre-Startup Safety Review (PSSR): For new or significantly modified facilities, conduct a safety review before introducing hazardous chemicals. The PSSR confirms that construction meets design specifications, procedures are in place, training is complete, and PHA recommendations are resolved.
- Mechanical Integrity (MI): Establish written procedures for maintaining the ongoing integrity of process equipment: pressure vessels, piping systems, relief valves, emergency shutdown systems, controls, and pumps. Inspections and testing must be performed to recognised and generally accepted good engineering practices (RAGAGEP).
- Hot Work Permit: Issue permits for hot work (welding, cutting, grinding) performed on or near covered process equipment. Permits must specify the work, equipment, and conditions that ensure the work is safe.
- Management of Change (MOC): Before making any change to process chemicals, technology, equipment, procedures, or facilities (except “replacement in kind”), conduct a formal review to identify new hazards, update PSI and procedures, and communicate the change to affected employees. MOC failures are one of the most common PSM violations.
- Incident Investigation: Investigate all incidents that did result in, or could reasonably have resulted in, a catastrophic release. Investigations must begin within 48 hours. A report including contributing factors and corrective actions must be prepared and retained for five years.
- Emergency Planning and Response: Establish an emergency action plan covering procedures for handling small releases. Coordinate with local emergency responders. Ensure alarm systems, emergency shutdown systems, and evacuation routes are functional and tested.
- Compliance Audits: Conduct compliance audits of all PSM elements at least every three years. Audit findings must be documented, addressed, and retained. Employers must certify that the audit was conducted and findings were resolved.
- Trade Secrets: Make all necessary PSI information available to employees, contractors, and OSHA regardless of trade secret status, subject to appropriate confidentiality agreements.
- Employee Participation: Develop a written plan for employee participation in PHAs and other PSM elements. Employees have the right to participate in PHAs and to access the required process safety information.
The Role of the OT Engineer in PSM
Automation and instrumentation engineers play a central role in at least four PSM elements:
- Process Safety Information: Maintaining current and accurate P&IDs is an OT responsibility. Outdated P&IDs are among the most common findings in OSHA inspections. Every configuration change must be reflected in the P&ID.
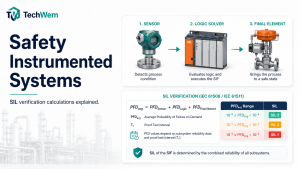
- Mechanical Integrity: Safety instrumented system (SIS) function testing, safety valve proof testing, and control valve stroke testing fall under MI. The testing frequency and acceptance criteria must be derived from the SIL verification study and the site MI programme.
- Management of Change: Any change to a PLC/DCS program that affects process control or safety — a setpoint change, a new interlock, a modified alarm — must go through MOC. Bypassing MOC for control system changes has been a contributing factor in multiple industrial incidents.
- Incident Investigation: When a process safety incident involves an instrumentation failure, a control system anomaly, or an interlock that failed to function, OT engineers are typically part of the investigation team. Root cause analysis tools such as Fault Tree Analysis (FTA) and barrier analysis are applied.
Common PSM Violations
OSHA cites these PSM violations most frequently:
- Failure to update P&IDs after plant modifications
- MOC procedures not followed for control system changes
- Mechanical integrity testing overdue or not documented
- PHA action items not resolved within agreed timelines
- Operating procedures not revised after process changes
These are engineering and management failures, not obscure compliance technicalities. A strong PSM programme is simply good engineering practice applied systematically to processes that can kill people if something goes wrong.